How do you evaluate the benefits of implementing predictive maintenance?
Don’t just look at “how many failures were caught”; understand the true ROI from 3 perspectives
After implementing Predictive Maintenance (PdM), what exactly counts as “effective”?
This may be a problem that many equipment managers and engineers have encountered.
The system is installed, the sensors have started collecting data, and we have indeed detected equipment anomalies several times.
But when the supervisor asks:
“So, after implementing it, how much did it actually save us?”
At times like this, it often isn't so easy to answer.
Because “detecting an anomaly” and “actually generating value” are really two quite different things.
If we only use “how many failures were caught” and “how accurate the diagnoses were” to evaluate predictive maintenance, it is easy to overlook its truly important value:
Let us know sooner what is happening with the equipment, and give us more time to decide what to do next.
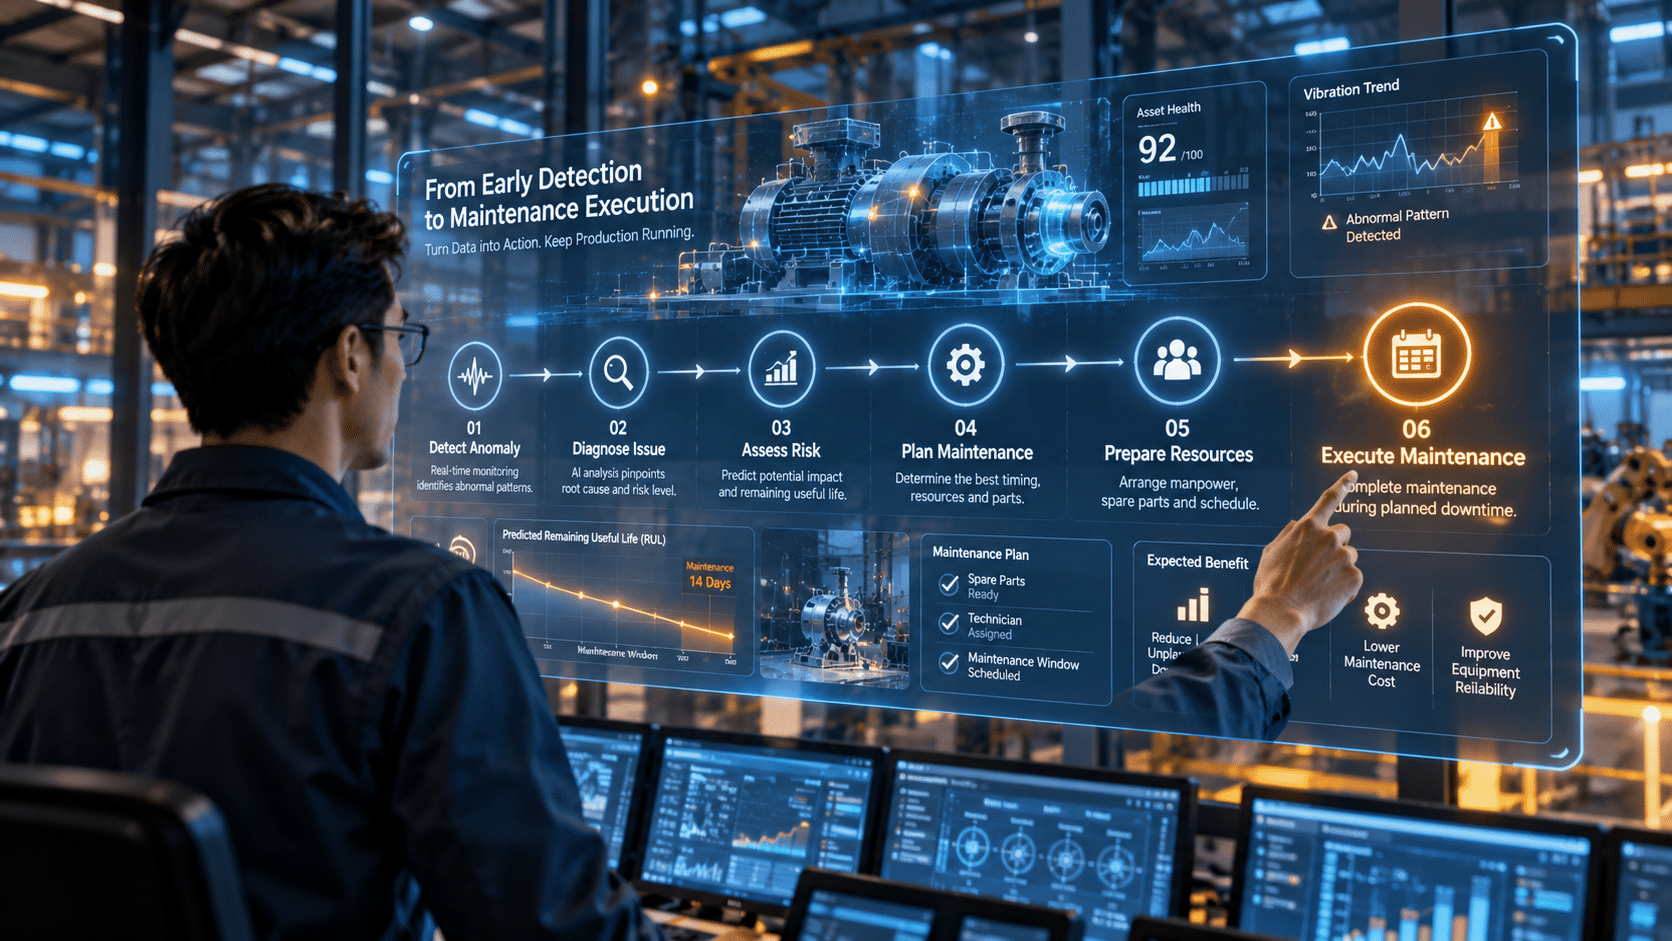
Detecting an anomaly does not mean you’ve already saved money.
We can think of equipment diagnostics as a health checkup.
Your health check tells you: “This value is a little abnormal, so you may want to keep an eye on it.”
This report is very important, but what truly affects your health is what you do after seeing the report.
Equipment maintenance is the same.
The system detected that bearing vibration is starting to increase and that the motor is showing abnormal signals, which means we are seeing problems earlier than before.
But if the equipment continues operating after receiving the alert and is only dealt with once it actually fails, then this early warning did not really change the outcome.
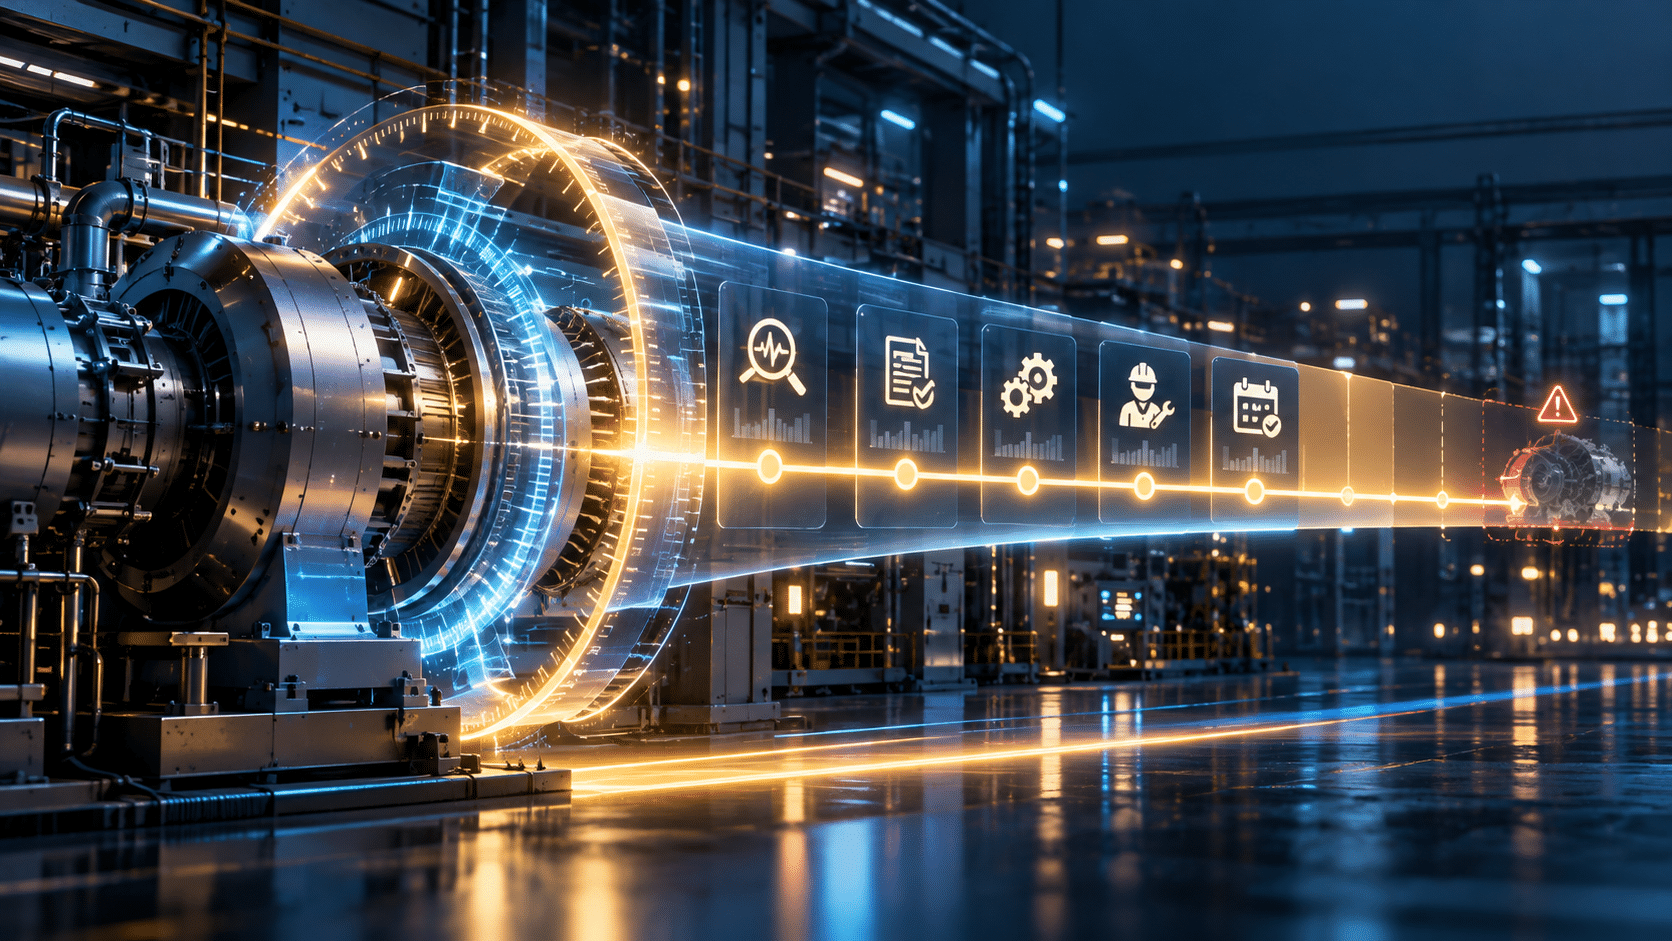
So, a complete predictive maintenance process should be:
Detect an anomaly → Confirm the issue → Assess the risk → Schedule maintenance → Prepare personnel and spare parts → Address it at an appropriate time
The key to truly creating value is not just “whether the system detects it,” but:
Has this information led us to make any maintenance decisions differently than before?
This is also a very important starting point when evaluating the benefits of predictive maintenance.
Before calculating ROI, you can first ask yourself 3 questions
When talking about predictive maintenance, it’s easy to start by thinking about calculating ROI.
But actually, before taking out the calculator, you can first take a look at the actual conditions at the equipment site.
Some equipment is well suited for predictive maintenance, while for other equipment, it may actually be more cost-effective to simply replace it when it breaks down.
Therefore, you can start with three simple questions.
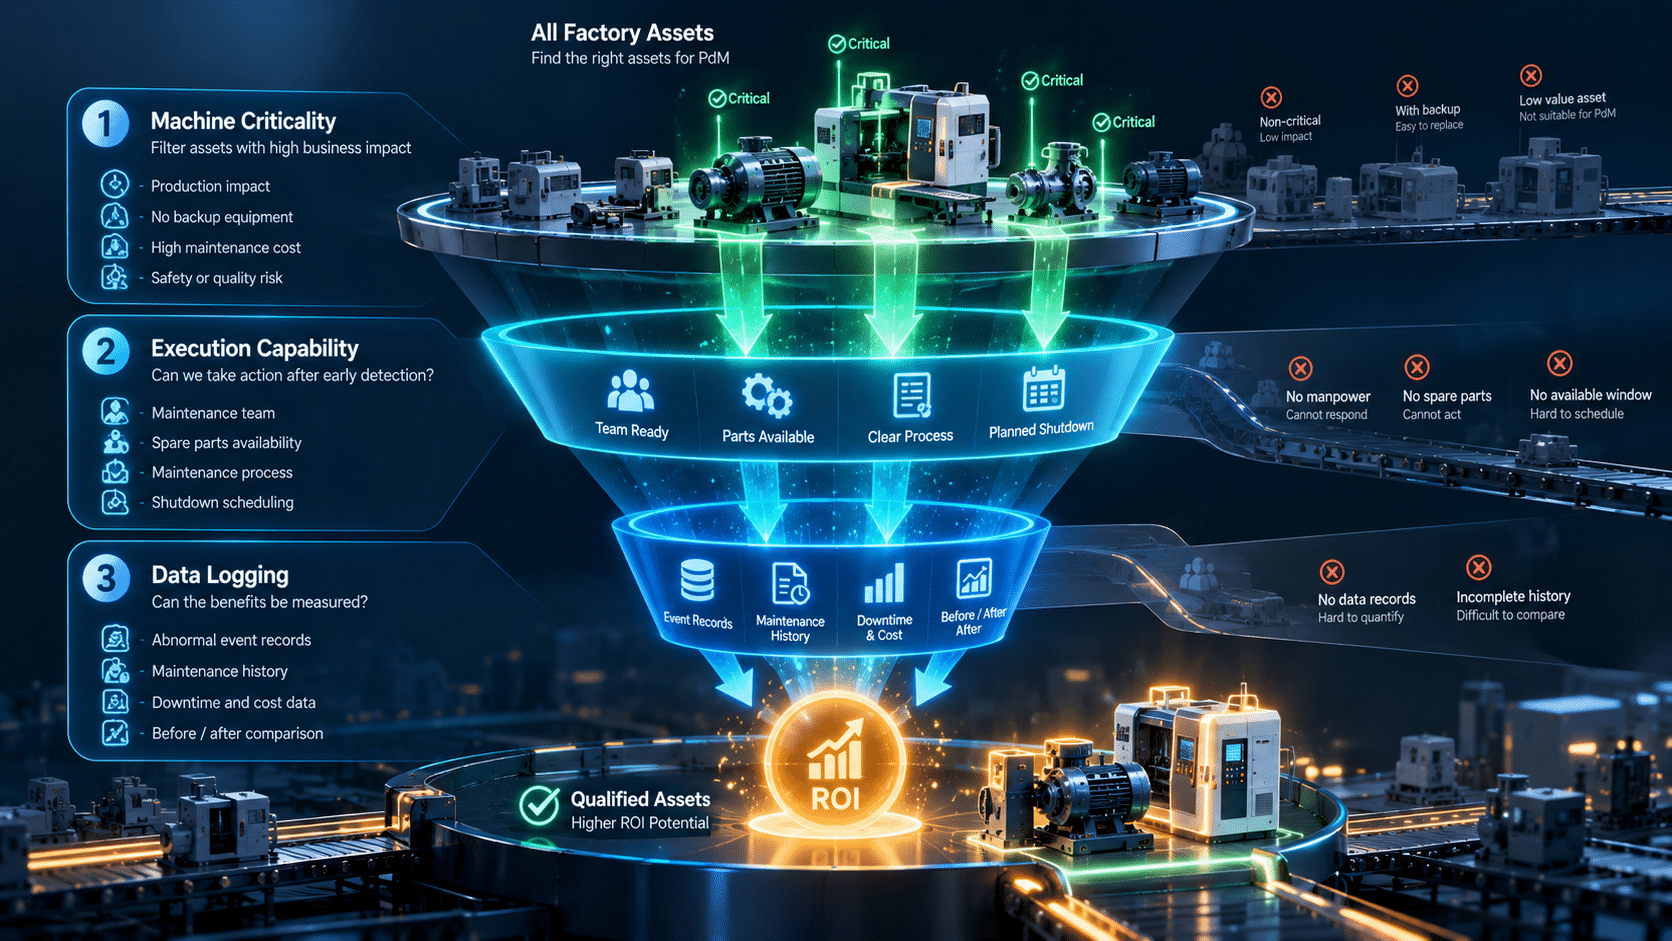
First question: If this equipment suddenly stops, would the impact be significant?
Not every piece of equipment needs predictive maintenance.
If it’s a low-cost piece of equipment with a spare available, and it can be replaced within half an hour if it breaks down, then investing a lot of resources in monitoring it may not be worthwhile.
But if today it’s a critical piece of equipment on a production line, a single shutdown can bring the entire upstream and downstream processes to a halt, and may even affect delivery schedules, then it’s a completely different story.
So you can think about it first:
Will the equipment shutdown affect production?
Is there any backup equipment?
How long will the repair take?
Are the parts difficult to obtain?
Once production is halted, will it affect quality or delivery schedules?
Generally, the more critical the equipment, the less redundancy it has, the longer the repair time, and the higher the cost of downtime, the more worthwhile it is to prioritize evaluating predictive maintenance.
Second question: What can we do after knowing in advance?
This question is actually more important than “how many days in advance can we issue a warning”.
Suppose the system is really powerful today and can tell you two weeks in advance:
“This bearing may be starting to have problems.”
Sounds great.
But if there are no spare parts on site, no maintenance personnel, and no suitable downtime window, then knowing two weeks in advance may ultimately still mean having to wait for it to break down.
So what really matters is not:
"How far in advance can I know?"
Rather:
“Now that we know in advance, is there anything we can do?”
For example, prepare the bearings in advance, arrange maintenance personnel, or coordinate with the production unit to schedule what could otherwise be an unexpected shutdown for the weekend or another time that has less impact on production.
This is when the value of predictive maintenance truly begins to emerge.
Third question: Have we recorded these benefits?
Many factories have actually avoided equipment failures by detecting abnormalities early.
Just ask again in six months:
“How much did we actually save that time?”
You may only remember:
"It seems like there was one time when the motor almost broke down."
The problem is that without leaving any data behind, it’s difficult to turn this into measurable benefits.
So there’s no need to establish a very complex system from the outset, but at the very least, you can retain a few basic pieces of information:
When did you notice something unusual?
What problem did you discover at the time?
What judgment did the maintenance personnel make?
Was maintenance arranged in the end?
What parts were replaced?
If it isn't handled in advance, how long might the downtime be?
How much did the repairs actually cost?
These seemingly basic records will actually be very helpful when it comes time to evaluate the benefits of PdM at the end of the year.
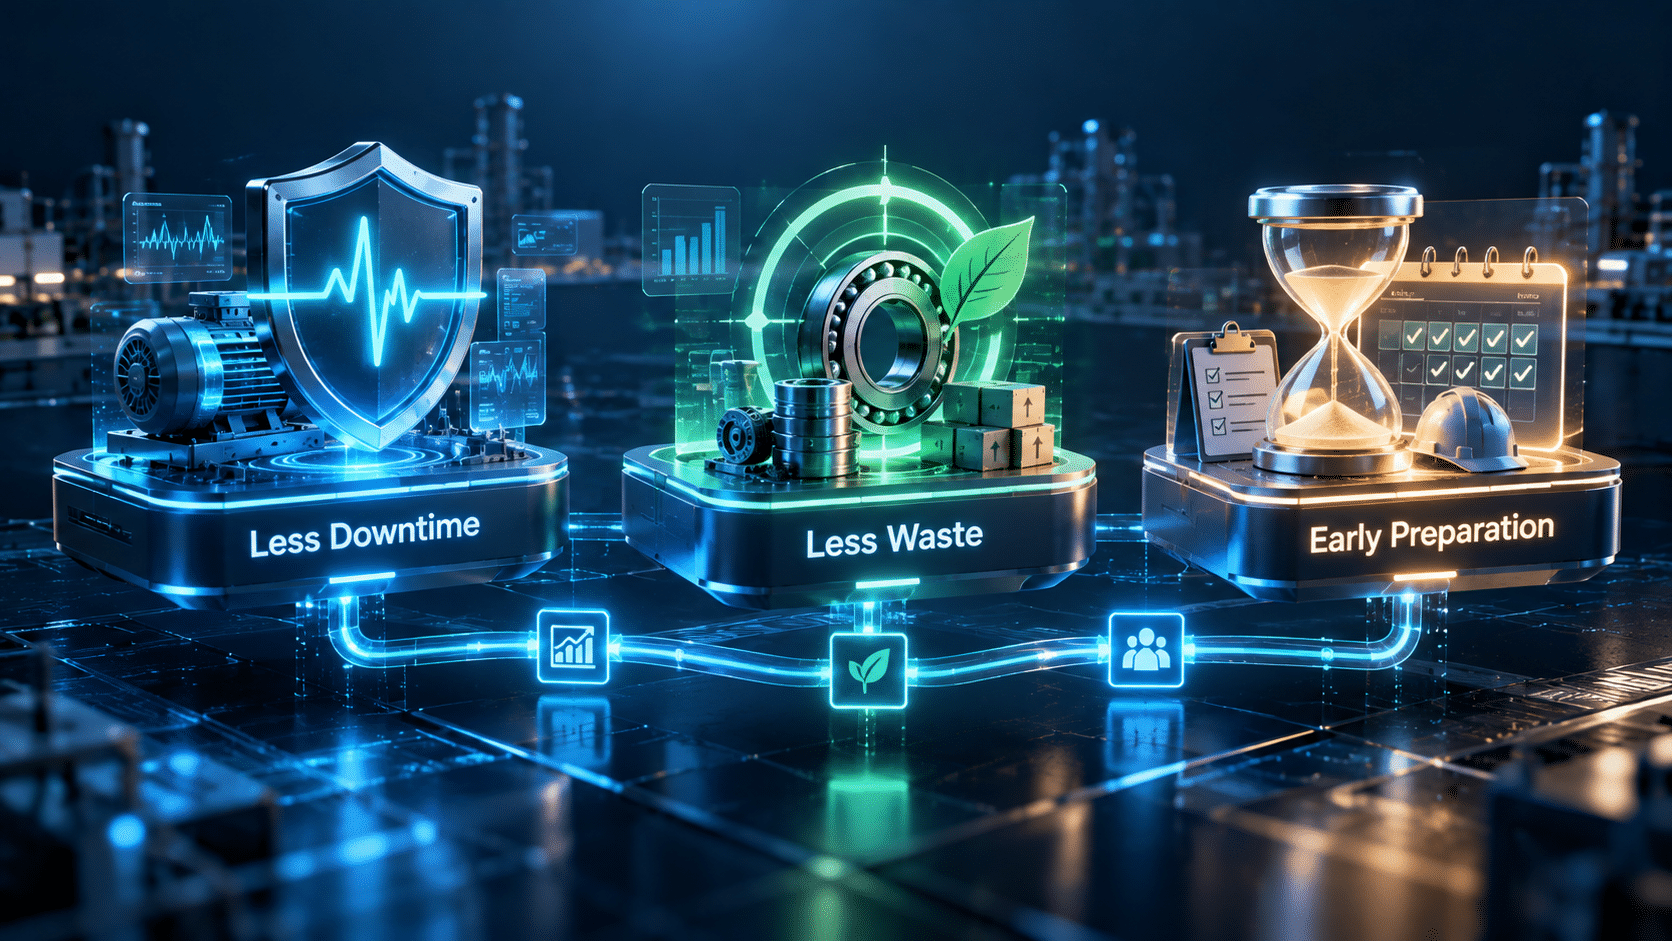
What benefits should predictive maintenance actually be evaluated on?
If we look at things more simply, we can examine them from three directions:
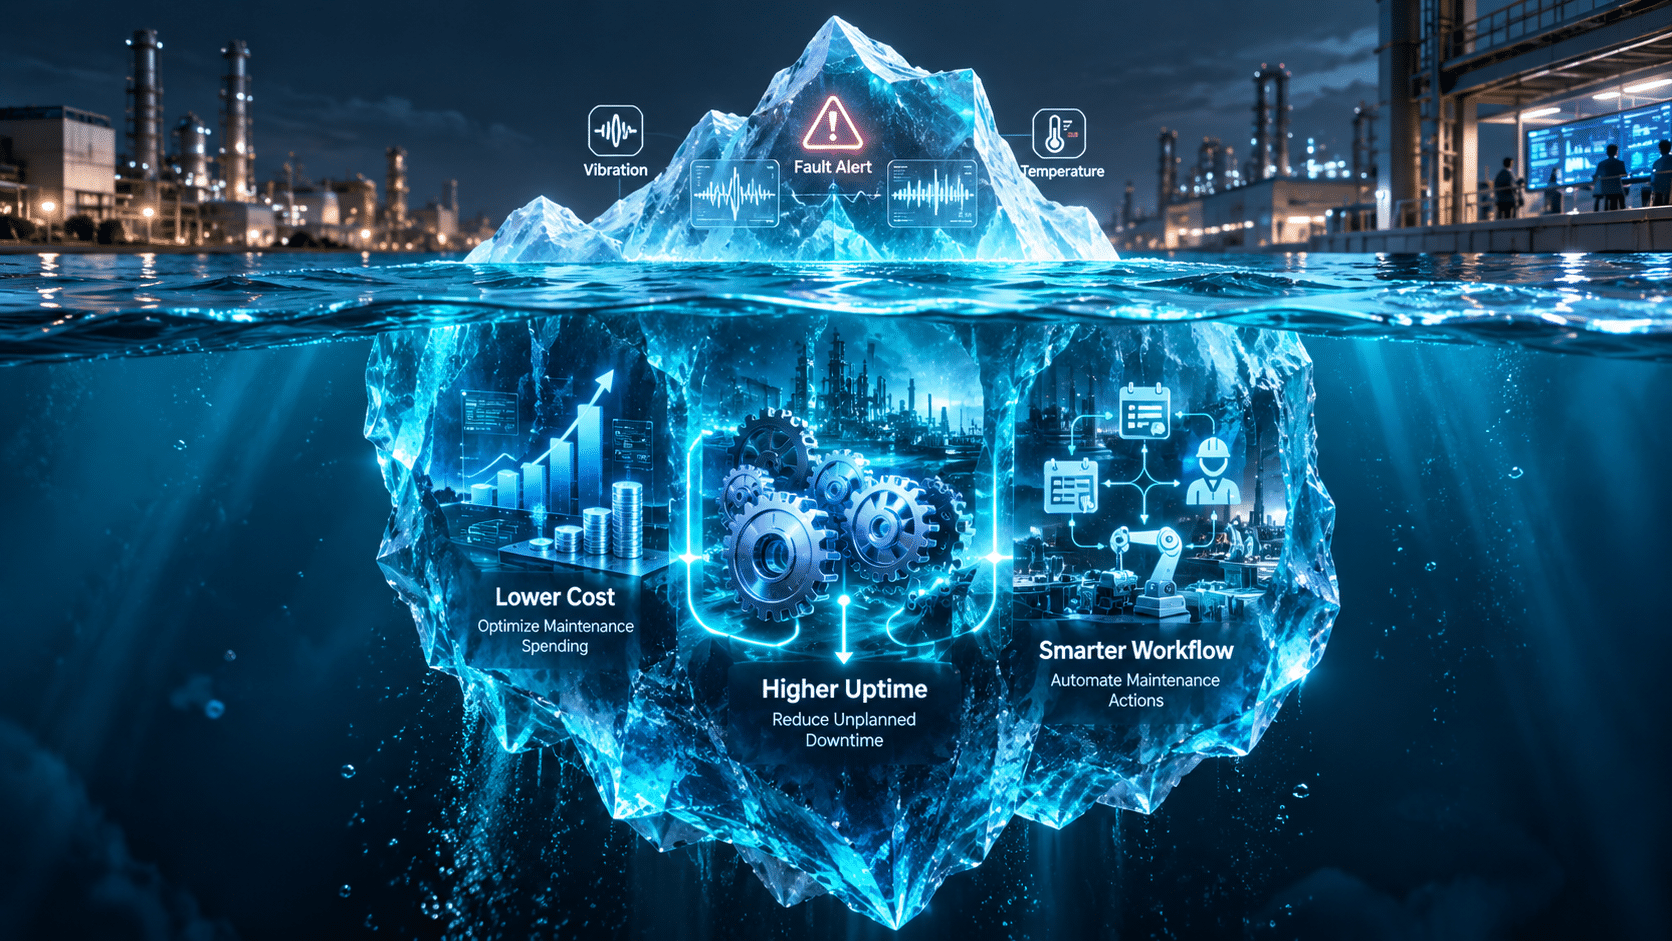
Less downtime, less waste, prepare a little earlier.
I. Less Downtime: Reduce the Risk of Unexpected Downtime
The truly costly part of equipment failures is often not the broken component itself, but the production interruptions, emergency repairs, and delivery impacts caused by downtime. Therefore, rather than focusing on “how many anomalies were detected,” it is more worthwhile to look at how many warnings were successfully converted into planned maintenance and how much unplanned downtime was actually reduced.
II. Waste Less: Reduce unnecessary maintenance costs
Although fixed-interval maintenance is convenient to manage, it may lead to usable components being replaced prematurely. Scheduling maintenance based on the actual health condition of equipment can reduce over-maintenance, emergency procurement, spare parts stockpiling, and unnecessary maintenance labor.
III. Prepare Early: Make Maintenance More Than Just Firefighting
The biggest benefit of detecting abnormalities early is having more time to prepare. The maintenance team can confirm the issue in advance, prepare parts, arrange personnel and downtime windows, and gradually shift from “rushing to repair equipment as soon as it breaks down” to “knowing where the problem is and having time to plan how to fix it.”
Therefore, when evaluating the benefits of predictive maintenance, it may be better to ask less often “how many failures were caught” and look more at: whether downtime has decreased, whether maintenance has become more precise, and whether the team has more time to prepare in advance.
Finally, don't just ask "how many failures were caught"
Accurate diagnosis is of course very important.
If even equipment abnormalities cannot be accurately identified, it will naturally be difficult for the subsequent benefits to materialize.
However, accurate diagnosis should be the starting point of predictive maintenance, not the endpoint.
The truly complete process should be:
See equipment status → Detect anomalies early → Assess risks → Change maintenance arrangements → Take action early → Reduce losses
So, next time you want to evaluate whether predictive maintenance is actually effective, don’t rush to ask:
“How many malfunctions have been caught this year?”
Could we replace them with three questions that are more closely aligned with the actual situation:
Aren't we missing some sudden shutdowns?
Did we perhaps do less unnecessary maintenance?
When the equipment really does have a problem, do we have a little more time to prepare than we used to?
If these three things all happen gradually, then what predictive maintenance brings is more than just a nice-looking equipment diagnostic report.
Instead, it gives the maintenance team more time to know, more time to prepare, and more options before the equipment actually stops.